Meaning
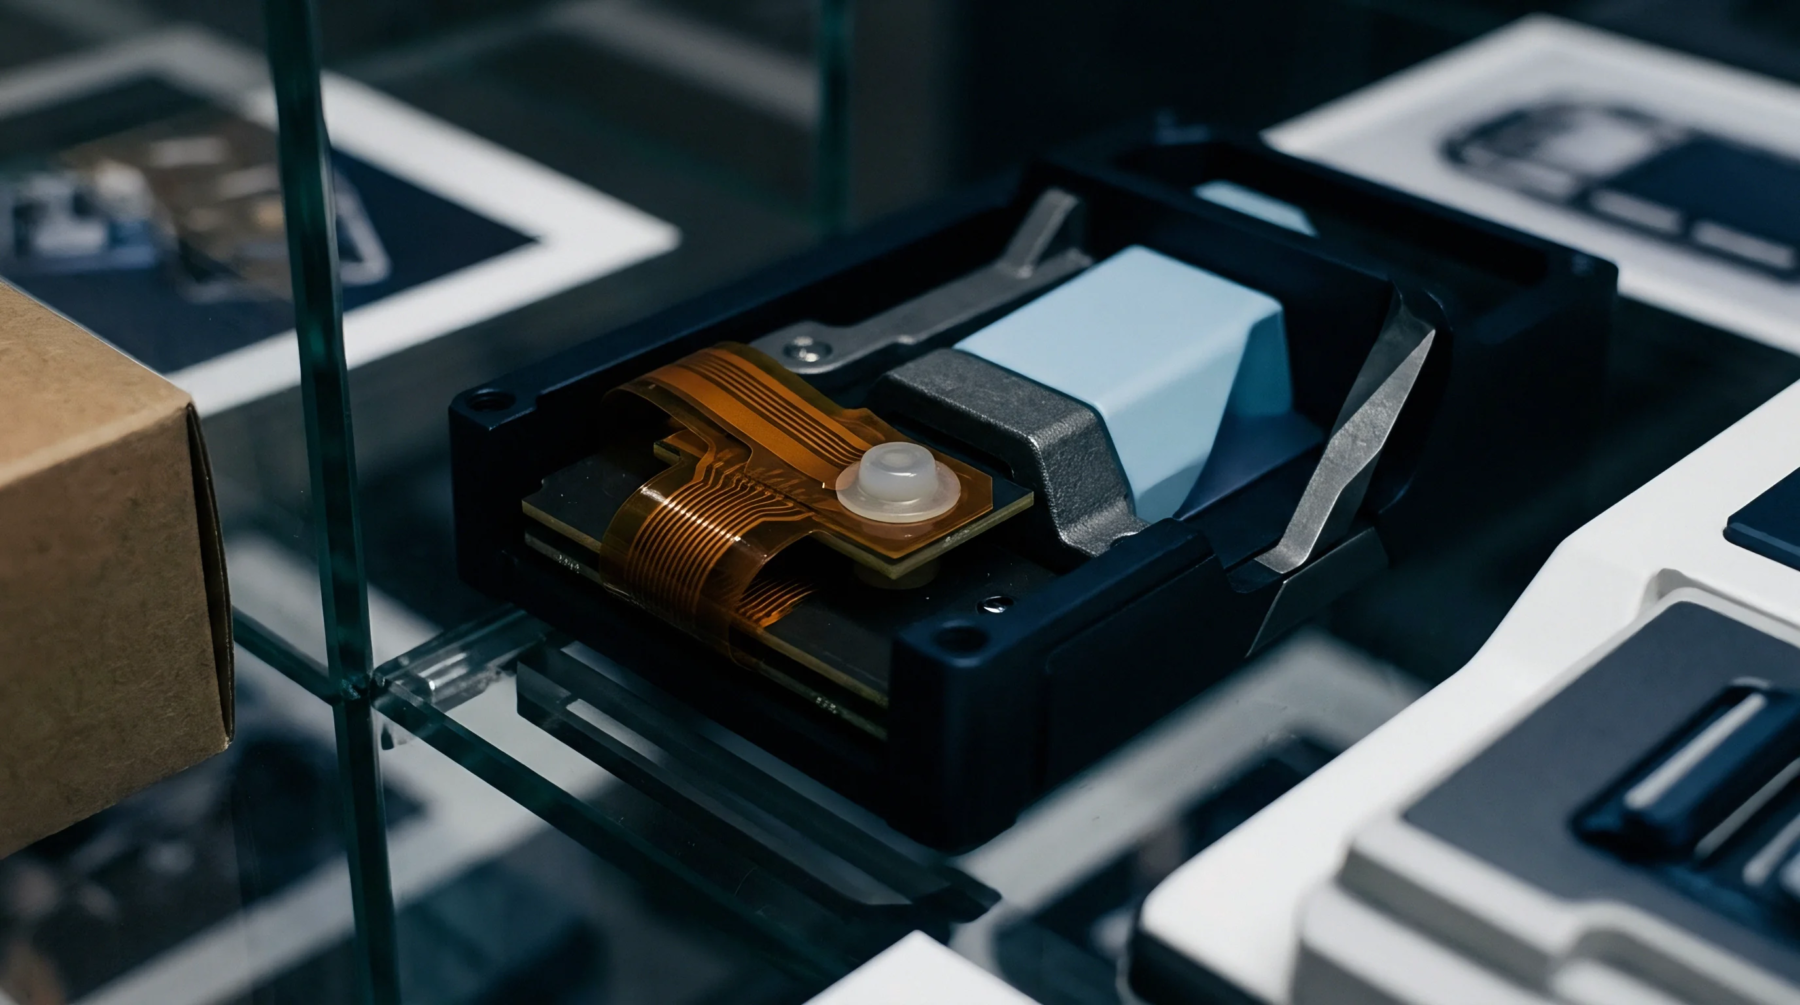
Custom verification equipment dedicated to validating physical radio frequency interfaces sits at the end of a production line. A target test harness physically receives a finished circuit board assembly, applies mechanical pressure to spring probes, and routes high frequency signals from vector network analyzers into the board under test. This specialized fixture enforces boundary conditions during final factory acceptance checks, halting the test sequence if insertion loss or return loss falls outside predetermined frequency limits.
Thermal Load
Dissipating heat during continuous high power transmitter verification requires dedicated thermal management built directly into the receiver baseplate. Active liquid cooling channels maintain ambient junction temperatures below eighty degrees Celsius while dummy loads absorb continuous wave signals. Thermal sensors monitor copper plate expansion during twenty minute soak cycles, compensating for dimensional shifts that would otherwise degrade coaxial contact repeatability.
Fixture Alignment
Physical registration depends on hardened steel guide pins locating against plated tooling holes on the radio frequency module. Mechanical wear on these alignment surfaces alters coaxial pin penetration depth, shifting insertion loss measurements by fractions of a decibel. Maintenance schedules specify replacement intervals for spring probes once contact resistance exceeds fifty milliophms across ten thousand insertion cycles.
Interface Tolerance
Manufacturing yield relies strictly on maintaining precise coaxial adapter coaxial concentricity between the test fixture and the device under production. Misalignment creates parasitic capacitance that distorts intermodulation distortion readings during multi carrier power amplifier characterization. Production engineers isolate fixture errors from device failures by running daily calibration standards through a known golden unit before certifying the assembly line for shift operations.