Quantifying Polymer Melt Velocity Gradients in High Temperature Tooling
Quantifying polymer melt velocity gradients requires combining Mooney wall slip slit die rheometry with non isothermal Cross WLF velocity profile modeling.
Viscosity
Aromatic high-performance polymers processed above three hundred fifty degrees Celsius exhibit pronounced non-Newtonian shear thinning across standard injection runner channels. Polyetheretherketone and polyphenylsulfone melts transition from Newtonian plateaus at low shear rates to power-law fluid behavior under operational tooling flow velocities. Quantifying the resulting velocity profiles across narrow flow channels demands explicit accounting of shear-dependent viscosity, temperature sensitivity, and boundary layer fluid slip along steel mold cavity faces.
Melt flow characterization under high shear rates relies on the Cross-WLF formulation to capture the combined effects of shear strain rate and temperature variance. The fluid viscosity scales dynamically with local shear rate according to the following analytical expression:
η(γ̇, T) = η₀(T) / (1 + (η₀(T) γ̇ / τ )1-n)
Zero-shear viscosity η₀(T) obeys the Williams-Landel-Ferry equation anchored at reference temperature Tr ~
η₀(T) = D₁ exp( -A₁ (T – Tr) / (A₂ + (T – Tr)) )
In these governing equations, γ̇ represents the local shear strain rate, τ defines the critical shear stress level marking the transition to shear thinning, and n is the power-law index. For neat PEEK 450G at a processing temperature of three hundred eighty degrees Celsius, typical regression parameters establish D₁ = 2.8 × 10⁴ Pa·s, τ = 1.5 × 10⁵ Pa, and n = 0.32. Shear rates near gate boundaries frequently exceed ten thousand reciprocal seconds, forcing fluid viscosity down by more than two orders of magnitude compared to core flow regions.
A runner dimension sized for standard polyolefins causes localized polymer thermal degradation when applied to high-temperature aromatic resins without adjusting for shear heating.
Velocity gradients across circular runner geometries derive directly from momentum conservation applied to the shear-thinning fluid model. For a channel of radius R subjected to axial pressure gradient dP/dz, the radial velocity profile u(r) incorporates both bulk non-Newtonian deformation and wall slip velocity us ~
u(r) = us + (R / (2 K))1/n (n / (n + 1)) (1 – (r / R)(n+1)/n) (dP/dz)1/n
Here K represents the fluid consistency index derived from local temperature fields. Velocity field calculations that assume zero wall slip produce errors in predicted pressure drop exceeding twenty percent when wall shear stress passes one hundred kilopascals. Viscous dissipation generates severe local temperature spikes within ten micrometers of mold steel boundaries.
Wall slip alters boundary shear. Ignoring fluid wall slip velocity distributions during high-temperature runner design leads to severe miscalculations in required clamping force, localized thermal degradation from unexpected friction heating, and invalid cavity filling predictions.

Die
Channel surface temperatures controlled via electrical cartridge circuits or pressurized oil circuits dictate fluid friction along mold boundaries. High-temperature tooling running polyetherketoneketone or polyamide-imide maintains wall temperatures between one hundred eighty and two hundred forty degrees Celsius. This substantial temperature offset between incoming melt bulk, often exceeding three hundred ninety degrees Celsius, and tool cavity steel creates a steep thermal boundary layer.
Viscous dissipation heating near channel walls competes directly with conduction cooling into the mold steel, altering local velocity gradients across the runner cross-section.

Runner Geometries and Wall Shear Dynamics
Cross-sectional fluid profiles transition from parabolic distributions to flattened plug profiles as injection rate increases. High shear stress at mold boundaries initiates fluid wall slip when shear stress passes material-specific thresholds. Melt fracture ruins aesthetic surfaces.
Shear rates peak near wall surfaces. The interaction between geometry, thermal boundary layers, and shear rate regimes governs filling behavior across micro-features and thin-walled cavity sections.
| Polymer Compound | Melt Temp (°C) | Tool Wall Temp (°C) | Power-Law Index n | Critical Slip Stress (kPa) | Peak Wall Shear Rate (s⁻¹) | Max Shear Temp Rise (°C) |
|---|---|---|---|---|---|---|
| PEEK 450G (Neat) | 385 | 195 | 0.32 | 140 | 42,000 | 28.5 |
| PEKK 6000 (Unfilled) | 375 | 205 | 0.29 | 125 | 38,000 | 31.2 |
| PPSU Radel R-5000 | 365 | 160 | 0.41 | 165 | 22,000 | 18.4 |
| PAI Torlon 4203 | 355 | 215 | 0.24 | 110 | 55,000 | 42.0 |
Thermal gradients across the flow channel alter local polymer density and shear capacity. High shear rates near channel walls reduce fluid viscosity, focusing flow velocity into a thin annular ring while core fluid moves as a pseudo-solid plug. Unquantified velocity profiles introduce severe defect mechanisms into molded components.
- Core voiding from skin-core freeze divergence emerges when rapid core velocity relative to stagnant outer boundary layers creates differential volumetric shrinkage during packing.
- Melt fracture along high-shear gate entry boundaries occurs when wall shear stress exceeds the cohesive shear strength of the high-temperature polymer melt.
- Uncontrolled mold flash caused by shear-induced thermal viscosity collapse happens when local frictional heating drops boundary viscosity below design limits near parting lines.
- Anisotropic fiber orientation in filled high-temperature compounds develops due to sharp velocity gradients aligning high-aspect fibers strictly parallel to runner faces while core fibers remain randomly oriented.

Thermal Boundary Layer Formation in Cartridge Tooling
Internal fluid temperature spikes emerge near mold channel margins through local mechanical energy dissipation. Brinkman number calculations quantify the ratio of viscous heat generation to boundary heat conduction:
Br = (η u²) / (k (Tm – Tw))
In high-temperature tooling processing PEEK at high injection velocities, Brinkman numbers regularly exceed two point five. Viscous dissipation generates internal heat. This indicates that mechanical shear heating dominates heat transfer over conductive cooling through cavity walls.
Consequently, localized fluid temperatures within boundary regions rise fifteen to forty degrees Celsius above set barrel delivery temperatures before melt reaches part cavities. Tooling fabricators frequently claim that uniform zone heating eliminates internal melt temperature variation, ignoring the physical reality of shear-induced thermal gradients within moving polymer streams.

Sensors
Quantifying velocity field variations inside high-temperature injection cavities relies on piezoelectric melt pressure transducers aligned along slit channels. Standard off-the-shelf instrumentation fails rapidly when exposed to continuous operational temperatures of two hundred degrees Celsius alongside melt stream contact temperatures reaching four hundred degrees Celsius. High-frequency inline ultrasonic pulse-echo velocity profiling and flush-mounted piezoelectric differential pressure sensors supply direct empirical data required to calculate wall shear stress and reconstruct channel velocity profiles.
In-Mold Ultrasonic and Slit Die Instrumentation
Acoustic wave propagation across high-temperature polymer streams yields real-time local velocity readings without disturbing melt fluid lines. High-temperature ultrasonic transducers fitted with specialized polyimide or quartz buffer rods launch multi-megahertz shear waves into moving polymer streams. Transducers monitor local channel pressure.
Echo signal delays provide spatial velocity mapping across runner channels with twenty-micrometer resolution.
- Drill flush-mounted transducer seats along the slit die flow path at fixed axial separation distances.
- Fit high-temperature quartz buffer waveguides flush with channel steel faces to preserve boundary fluid flow lines.
- Expose piezo-ceramic sensing elements to controlled thermal oil circuits to maintain transducer casing temperatures below eighty degrees Celsius.
- Record high-frequency acoustic echo profiles across full injection stroke durations using dedicated ten-bit digitization hardware.
- Extract local Doppler frequency shifts to calculate velocity vectors as functions of radial distance from channel centerline.
Tooling integration contracts referencing ISO 11443 for capillary rheology require temperature stability within half a degree Celsius across all pressure transducer seats during active flow.
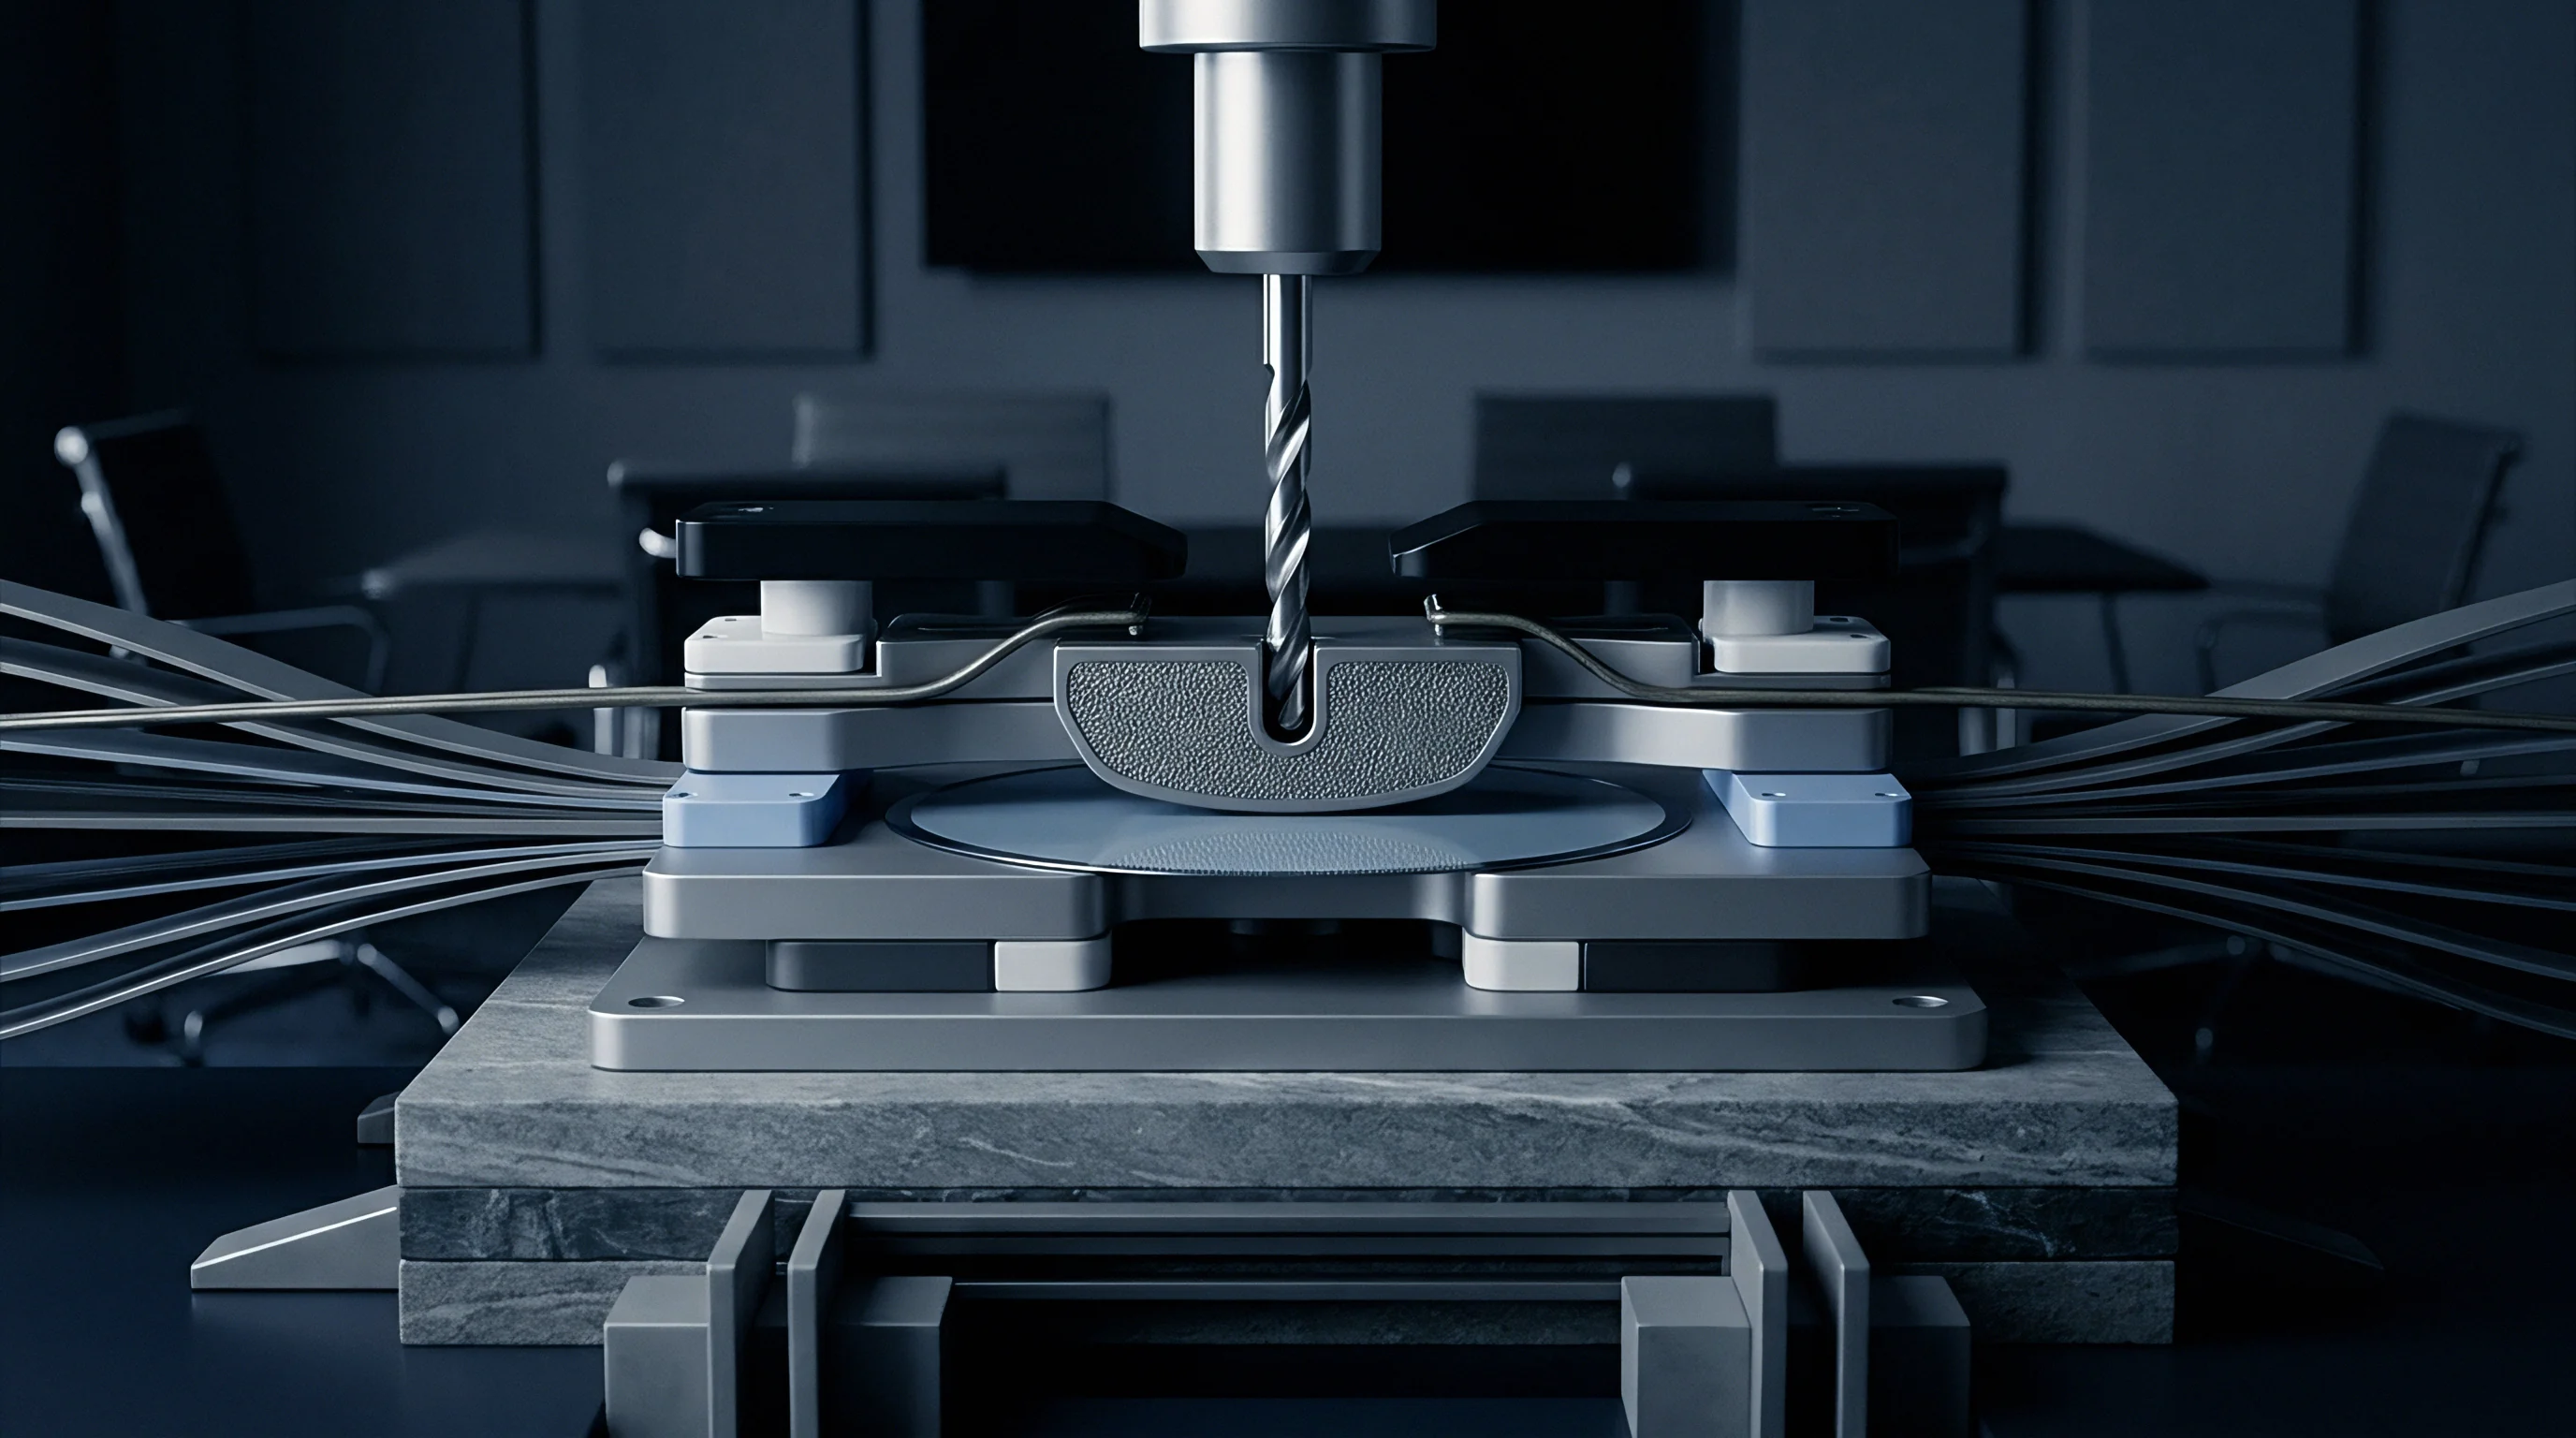
Sensor Calibration Scope and Tooling Hardware Integration
Piezoelectric pressure devices mounted inside mold cavity blocks demand multi-point thermal zero-drift corrections before production trials start. Thermal expansion of transducer housing assemblies shifts zero-point voltage offsets by up to eight percent of full-scale reading when heating tools from ambient to two hundred degrees Celsius operational targets. Calibration curves prevent signal drift.
Consider an engineering scope contract specifying in-situ melt velocity gradient characterization for a four-cavity high-temperature runner system. Sensor hardware non-recurring engineering costs break down across transducer hardware, signal conditioning electronics, custom machining, and data acquisition firmware development. A dual-location slit die configuration utilizes four high-temperature pressure transducers rated to four hundred fifty degrees Celsius and two ultrasonic buffer probes.
Transducer procurement and thermal waveguide fabrication require twelve thousand five hundred dollars. Custom spark-erosion machining for flush sensor seats inside hardened CPM-10V tool inserts adds six thousand eight hundred dollars. High-speed signal acquisition hardware capable of simultaneous one-hundred-megahertz acoustic sampling costs fourteen thousand two hundred dollars.
Calibration software development and regression module integration add eight thousand five hundred dollars in engineering labor. The complete measurement package adds forty-two thousand dollars in upfront non-recurring costs. Skip this instrumentation expenditure and boundary velocity profiles must be estimated using unvalidated capillary rheometer handbooks, introducing unpredictable dimensional variations into final product geometry.
Purchase orders for high-temperature tooling modules executed under ASTM D3835 or ISO 11443 compliance clauses require certified multi-point thermal zero-calibration matrices delivered as part of initial tool handover documentation.
Modeling
Computational fluid dynamics formulations for semi-crystalline aromatic polymers require empirical non-isothermal rheological parameters derived under production strain rates. Standard commercial molding software defaults to simplified isothermal models that fail to capture boundary layer velocity gradients in high-temperature tooling. Accurate prediction of fill patterns, gate freeze times, and cavity pressure evolution demands explicit numerical coupling between temperature fields, shear-thinning viscosity, and stress-induced wall slip velocity.

Mesh Boundary Refinement for High-Shear Gradients
Discretization nodes concentrated within fifty micrometers of metal mold channel surfaces capture extreme local strain rate variations. Coarse finite element meshes miss viscous heating spikes along walls, producing underpredictions of local flow speed. Element aspect ratios within boundary mesh layers require maintenance below five to one to maintain numerical convergence in high-gradient domains.
| Simulation Model Formulation | Wall Slip Integration | Boundary Layer Mesh Density | Predicted vs Actual Delta P (%) | Velocity Profile Error (%) | Computational Overhead Ratio |
|---|---|---|---|---|---|
| Isothermal Power-Law | None (Zero-Slip) | Coarse (0.5 mm) | +28.4 | 34.2 | 1.0x |
| Non-Isothermal Cross-WLF | None (Zero-Slip) | Medium (0.1 mm) | +18.6 | 21.5 | 3.8x |
| Non-Isothermal Cross-WLF | Mooney Linear Slip | Fine (0.01 mm) | -3.1 | 4.2 | 12.4x |
| Temperature-Dependent Cross-WLF | Non-Linear Slip Threshold | Adaptive Boundary Layer | -1.2 | 2.1 | 18.6x |
Refining finite-element boundary layers captures sharp shear rate spikes near cavity steel interfaces. Melt temperature governs initial fluid viscosity. Uncorrected models understate gate resistance.
Simulations omitting Mooney wall slip overestimate runner pressure drops by twenty-four percent at shear rates above ten thousand reciprocal seconds.
Simulations omitting Mooney wall slip overestimate runner pressure drops by twenty-four percent at shear rates above ten thousand reciprocal seconds.

How Does Wall Slip Shift Rheological FEA Calibration?
Fluid detachment at steel mold boundaries alters standard pressure drop predictions across narrow runner gates. Mooney wall slip analysis quantifies true bulk shear rates by evaluating apparent shear rates across multiple die capillary diameters. Apparent shear rate γ̇a relates to true wall shear rate γ̇w and wall slip velocity us through channel radius R ~
γ̇a = (4 Q) / (π R³) = γ̇w + (4 us) / R
Plotting γ̇a against 1/R at constant wall shear stress yields slip velocity us directly from line slopes. Incorporating this wall slip coefficient into finite element simulations resolves discrepancies between calculated filling pressures and physical cavity transducer logs. Whether non-isothermal boundary layer stress relaxation rates alter localized polymer orientation distributions during ultra-high-speed injection remains an open question in current micro-molding rheology research.


Tooling
Specification packages for high-temperature injection molds set clear ownership boundaries for physical hardware, rheological simulation files, and sensor signal conditioning systems. High-temperature tooling running continuous production above two hundred degrees Celsius utilizes specialized tool steel alloys such as CPM-10V or premium H13 treated with titanium nitride surface coatings. Sourcing contracts must clearly specify whether non-recurring engineering charges cover characterization software firmware, raw transducer calibration matrices, and CAD files for custom slit-die inserts.

Commercial Scope Division and Design Transfer Deliverables
Turnkey procurement agreements state exact responsibilities for mold core fabrication, transducer calibration, and melt flow software file handovers. Disagreements arise when buyers assume mold development fees include full access to raw sensor calibration code and custom simulation mesh files, while tooling vendors treat those assets as proprietary intellectual property. Defining explicit deliverable schedules inside supply contracts prevents expensive scope disputes during second-source manufacturing transfers.
- Native 3D CAD models of flow runners and sensor cavities formatted as unencrypted STEP or IGES files detailing exact runner steel geometry and insert tolerances.
- Raw rheological characterization raw files and WLF regression coefficients generated from capillary and slit-die testing for the specific resin lot used during qualification.
- Calibration curves for embedded high-temperature piezo-transducers including multi-point thermal zero-drift matrices certified across full operational temperature ranges.
- Firmware source code for real-time ultrasonic velocity processing units enabling independent maintenance, modification, and recalibration without original vendor lock-in.

Non-Recurring Engineering Amortization and Tooling Ownership
Initial development expenditures convert directly into unit price adjustments when high-temperature mold manufacturing scopes split hardware build from characterization testing. Standard high-temperature single-cavity prototype tooling running PEEK compounds costs sixty-five thousand dollars for basic mechanical build. Adding custom slit-die sensor ports, high-frequency ultrasonic waveguides, and inline pressure characterization increases initial non-recurring engineering charges to one hundred seven thousand dollars.
Tool steel choices dictate mold life. Simulation files define gate dimensions. Contract clauses assign financial exposure.
Tooling transfer packages that exclude raw transducer calibration tables force buying engineers to re-qualify mold cavities at secondary production facilities.
Amortizing characterization costs over small production runs drastically alters unit economics. On a ten-thousand-unit initial run, unamortized instrumentation NRE adds ten dollars and seventy cents per part. Amortizing hardware across one hundred thousand units reduces instrument burden to one dollar and seven cents per piece.
Tooling integration agreements defining scope transfers must include explicit acceptance clauses verifying velocity gradient alignment between numerical simulation models and physical transducer outputs prior to final bill-of-materials capital disbursement. A mold that passes dry mechanical dry-cycle checks but fails velocity gradient symmetry requirements remains incomplete until the toolmaker modifies runner balances at their own expense.