Meaning
A non-exhaustive quality assurance protocol evaluates discrete product assemblies or sub-components at random intervals during a high-volume manufacturing run to detect latent assembly flaws before final pack-out occurs. Spot check verification functions as a statistical control mechanism that identifies variances in mechanical alignment or interface tolerances within a production batch without requiring the total inspection of every unit. This process relies on the extraction of a subset from a larger population to infer the reliability of the output quality across the entire line.
The method finds its primary application in radio frequency modules where manual adjustments to antenna positioning or grounding spring compression often drift during long shifts. By sampling a specific quantity of finished devices at preset intervals, the line operator gathers data regarding the frequency of soldering defects or connector misalignment. The boundary of this operation exists where the failure rate of the sample reaches a predetermined threshold, at which point the line stops for calibration and the entire batch undergoes full screening.
It provides an immediate feedback loop for manufacturing engineers who track the drift of automated assembly tools.
Sampling Protocol
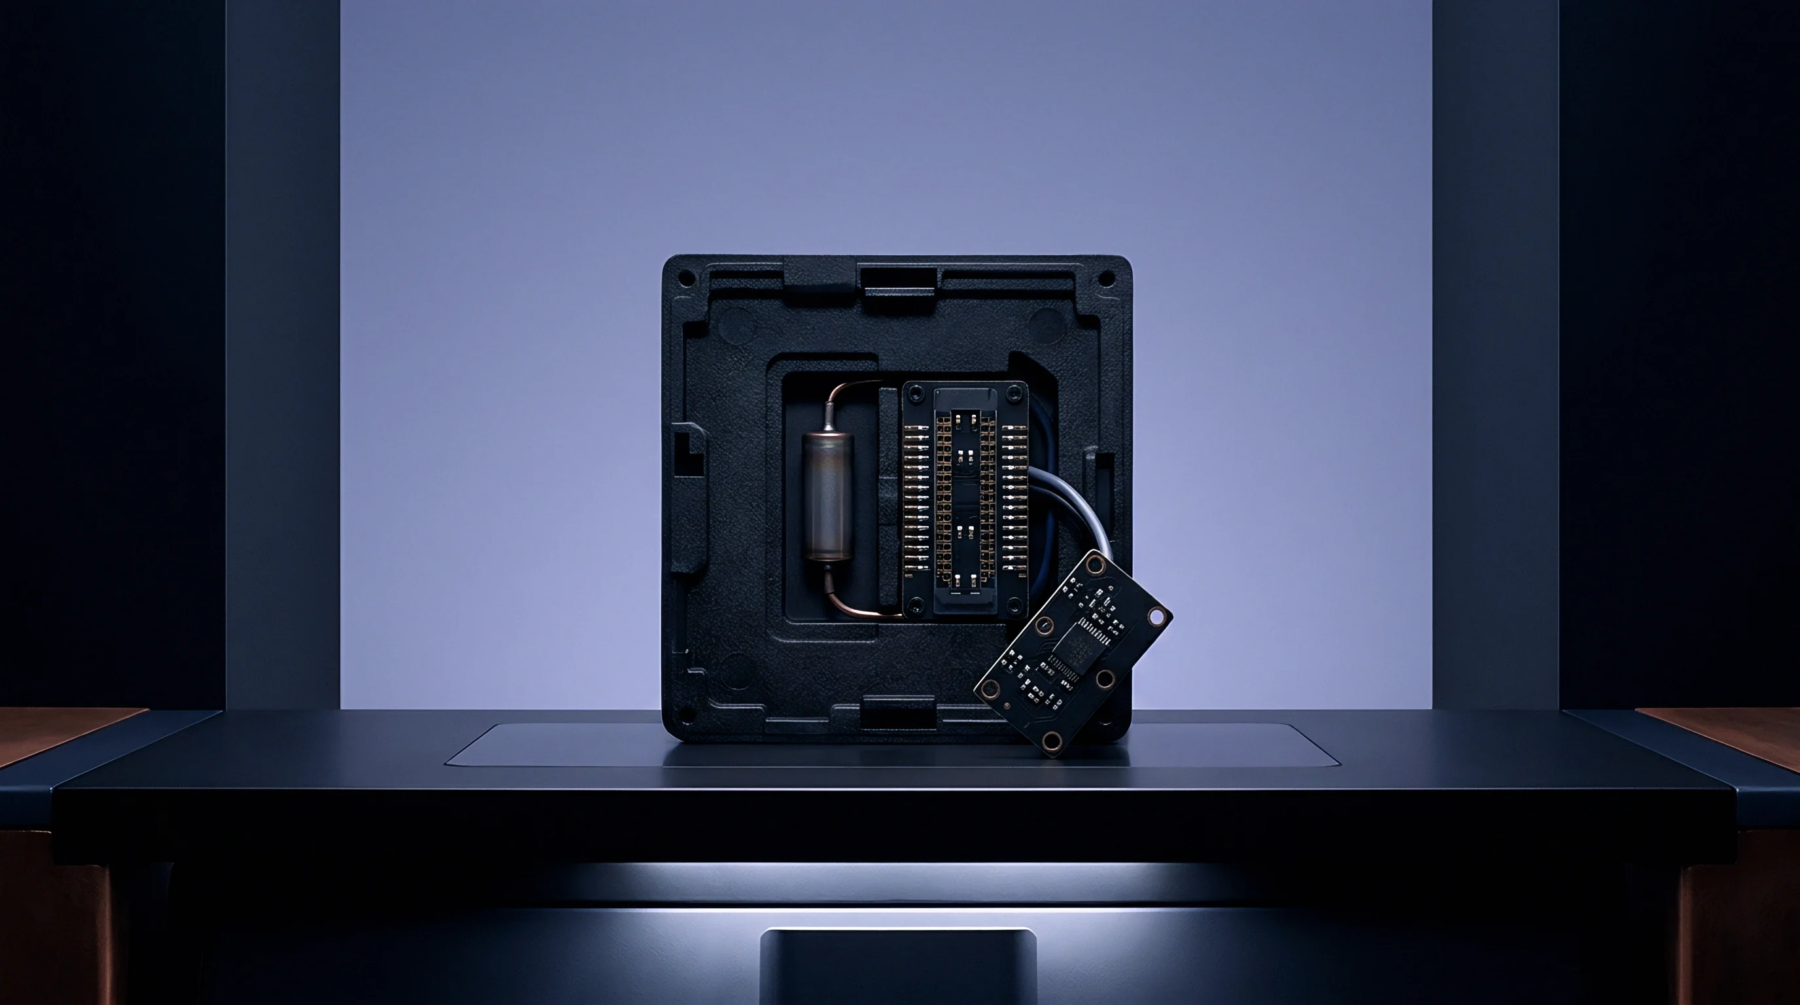
Operators pull units for this assessment from the conveyor belt based on a pre-defined interval or every thousandth unit produced. The procedure necessitates a check of mechanical dimensions using a calibrated jig to ensure that the printed circuit board remains centered within the housing. Engineers record the results of these checks on a control chart to monitor if the tool wear trends toward a tolerance violation.
When the sample indicates a measurement near the edge of the allowed range, the team adjusts the automated pick and place equipment before the actual production output crosses the rejection line.
Quality Threshold
Each instance of an out of tolerance measurement triggers an automatic audit of the preceding units since the last recorded pass. Management defines these thresholds by calculating the maximum allowable variance that the enclosure can accommodate without impacting the final transmission performance or the user experience of the modular hardware. If the sample reveals a pattern of degradation in the mechanical fit, the production team segregates all items produced since the last successful check.
The absence of a failure in these checks provides sufficient confidence to proceed with the shipment of the remaining production volume.
Operational Performance
Maintaining this practice reduces the overhead costs associated with total inspection while protecting the supply chain from the influx of non-conforming items. Precision in the selection of the sample size determines the reliability of the conclusion drawn about the total batch quality. Tightened constraints on sampling frequency provide a faster response to tool drift but increase the overhead of the monitoring staff.
Small batches or high value assemblies often necessitate a smaller interval between these tests to mitigate the financial impact of potential rejects. A stable measurement of sample consistency proves that the manufacturing line operates within its designed mechanical envelope.