In-Circuit Test Vector Synthesis for High Density Assembly Modifications
Vector synthesis for modified assemblies requires delta netlist verification, BSDL timing re-validation, and algorithmic backdrive current bounds.

Boundary
Modifying a high-density printed circuit board alters conductor routing and component footprints without adding target area for test probes. When an engineering change order (ECO) adds trace cuts, jumper wires, micro-vias, or tight-pitch component re-spins to a dense assembly, standard physical test points disappear. Bed-of-nails fixtures that depend on 1.0 millimeter or 0.8 millimeter probe target pads run into physical interference whenever component clearances fall below 0.35 millimeters.
In-circuit testing (ICT) requires nodal isolation to force known voltage states, measure individual component impedance, backdrive digital gates, and catch manufacturing defects like solder bridges or unbonded pins. Without direct physical node access, static test vector sets written for the baseline layout fail during execution, producing false failures or unisolated faults.
Node Density and Physical Access Collapse
Surface-mount geometries below 0.4 millimeter pitch leave no room for the dedicated copper lands traditionally assigned to bed-of-nails spring contacts. When physical test pads are removed to clear routing channels for modified multi-layer traces, electrical nodes go unprobed. Test vector synthesis then has to adapt to partial-access topologies, energizing digital and analog nodes indirectly through adjacent silicon ICs or through flying probe contacts operating with reduced contact force.
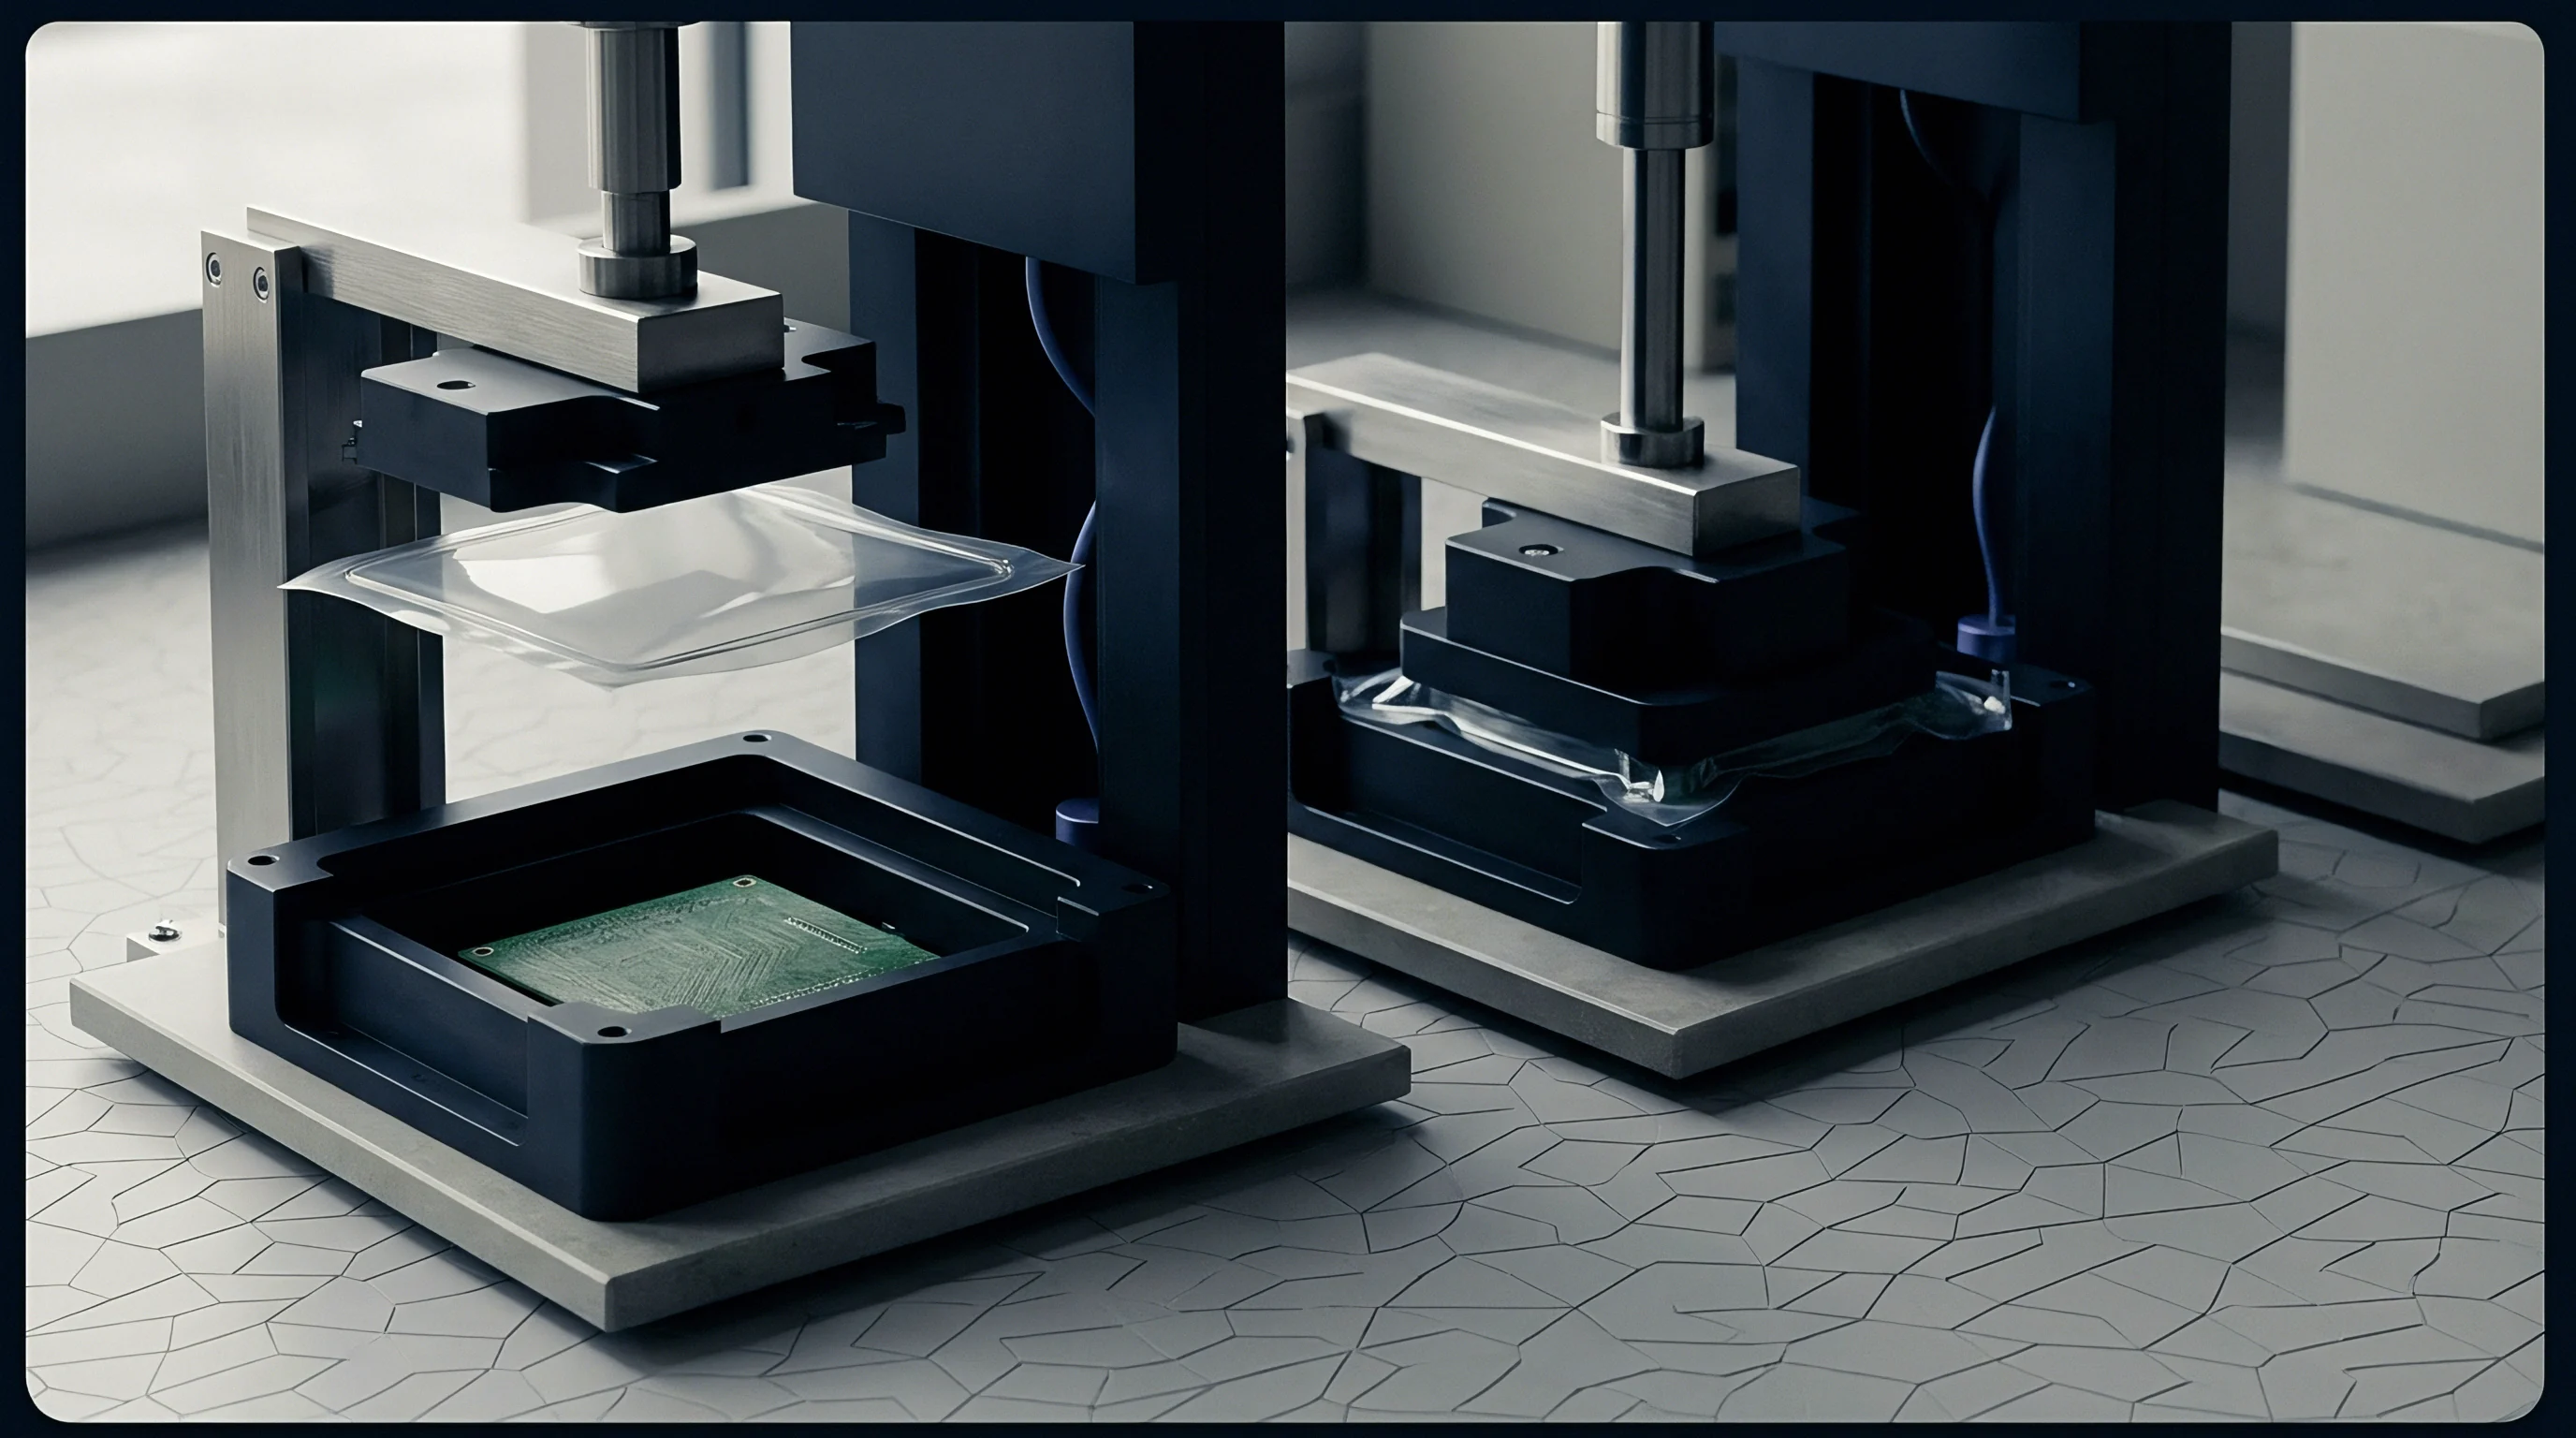
Flying probe systems bypass fixed-fixture limits by moving motorized test needles across fine-pitch features. Probe positioning tolerances down to 15 micrometers allow contact with exposed micro-vias or component termination lands. A high-density assembly with 4,000 nets probed entirely by flying heads takes over eight minutes per board, compared to twelve seconds on a dedicated bed-of-nails fixture.
Synthesizing test vectors for modified high-density boards therefore requires balancing physical probe access against algorithmic vector generation to keep defect detection high without bottlenecking line throughput.
Backdrive currents exceeding 250 milliamperes applied for longer than 12 milliseconds cause junction temperatures in unbuffered CMOS outputs to surpass 150 degrees Celsius.

Netlist Delta Tracking across Rapid Re-Spins
Engineering change orders generated during mid-production prototype revisions introduce discrepancies between layout databases and schematic capture files. Generating test vectors from an outdated netlist results in incorrect probe pin assignments and improper backdriving sequences. Automated vector synthesis tools rely on CAD extraction files that explicitly flag modified nets, added component bodies, and severed signal lines.
Netlist delta reconciliation compares the original layout parasitic database against the post-modification CAD netlist. The synthesis tool categorizes each net as fully probed, partially probed, or unprobed. For unprobed nets, vector synthesis algorithms must rely on boundary-scan structures or functional cluster stimulus to infer structural continuity.
Skipping netlist delta reconciliation leads to aborted test program executions and invalid fault dictionaries.
Running unverified vector models after modifying a high-density assembly risks leaving solder bridges untested, net opens unisolated, and active silicon gates physically destroyed during end-of-line testing.


Trace
Rerouting signal lines on high-density assemblies alters physical impedance and electrical length between active component pins. Cut traces and modification jumpers shift propagation delays, crosstalk coupling, and backdrive transient responses. Automatic test vector synthesis engines account for these variations by adjusting drive edge timings and sensing voltage thresholds during structural vector execution.
BSDL File Validation for Modified Silicon
Boundary scan description language (BSDL) structures describe internal shift registers and I/O cell behavior in programmable integrated circuits. Swapping a silicon device for a pin-compatible variant or altering board strap configurations renders the original BSDL file invalid. Synthesizing boundary scan test vectors requires exact alignment among physical silicon IDCODES, instruction register lengths, and boundary register cell maps.
Validating BSDL files against modified assembly netlists involves parsing instruction sets, verifying compliance with IEEE 1149.1 and IEEE 1149.6 standards, and remapping boundary cells to the revised net layout. If an ECO redirects a boundary-scan cell signal through a physical trace cut to an external jumper, the vector generator recalculates shift paths to prevent illegal driver bus contention.
Without proper BSDL validation, solder bridges remain undetected.

Cluster Test Pattern Generation Mechanics
Non-scannable glue logic and analog peripherals positioned between boundary-scan ICs require algorithmic stimulation through adjacent digital nodes. Cluster vector synthesis builds sequential digital patterns driven from boundary-scan outputs, routing them through non-scannable components and reading results back at receiving boundary-scan input cells.
| Test Methodology | Physical Pad Target Required | Average Fault Coverage | Diagnostic Isolation Depth | Execution Speed Per Board |
|---|---|---|---|---|
| Full-Access Bed-of-Nails ICT | 100% of Circuit Nets | 96.5% to 99.1% | Single Pin or Component | 8 to 15 Seconds |
| Partial-Access Hybrid ICT | 45% to 70% of Circuit Nets | 82.0% to 89.5% | Component Cluster or Net Pair | 12 to 25 Seconds |
| Boundary Scan ATPG (IEEE 1149.1/6) | 0% (Uses Silicon Scan Chain) | 68.0% to 78.4% | Boundary Register Cell | 3 to 8 Seconds |
| Flying Probe with Vector Synthesis | 15% to 35% Micro-Via Contact | 88.5% to 94.2% | Sub-Net or Component Level | 180 to 450 Seconds |
Resynthesizing cluster patterns after physical board modifications requires a structured verification sequence to prevent backdrive collisions and gate damage:
- Import updated CAD netlist files and post-modification Gerber layout databases into the ATPG workspace.
- Extract modified BSDL files for replaced or reconfigured integrated circuits, confirming boundary cell register length compatibility.
- Run automated net access analysis to categorize nets into direct probe points, boundary-scan driven nets, and unprobed clusters.
- Generate truth tables for non-scannable cluster logic using surrounding boundary-scan cells as virtual drivers and receivers.
- Simulate current draw during backdriving pulses to verify output driver thermal dissipation stays within safe bounds.
- Validate generated test vectors against physical golden boards using a flying probe system or modified fixture receiver.
IPC-2591 Section 4.2 mandates that layout modification files supply node-level netlist deltas, failing which automated vector synthesis reverts to full-board re-generation.
Standard manufacturing master services agreements include a test-coverage retention clause: any engineering change order causing more than a two percent drop in structural fault isolation voids the factory first-pass yield warranty.


Vector
Algorithmic pattern generation translates physical structural tests into timed logic sequences applied at available board nodes. As high-density modifications reduce physical pin access, test vector synthesis must shift from direct nodal measurement to algorithmic state excitation. Vector synthesis engines model logic propagation across active components, ensuring digital patterns toggle every accessible internal gate while preventing uncontrolled outputs.

Does Reduced Pin Access Compromise Backdrive Thermal Safety?
Overdriving operational logic states on node lines forces upstream output transistors to source or sink current well beyond normal operating ratings. While direct physical access allows test systems to isolate nodes cleanly, restricted probe access forces vector generators to backdrive upstream gates through intermediate logic paths, extending backdrive duration across connected silicon devices.
Backdrive current depends on driver technology, output stage impedance, and junction temperature. A typical low-voltage CMOS output transistor draws between 150 and 350 milliamperes when forced into an opposing logic state, and backdrive pulses longer than 10 to 12 milliseconds cause rapid localized heating on unbuffered lines. To prevent thermal damage, automated vector synthesis algorithms restrict backdrive pulse windows to under 2 milliseconds and insert cooling pauses between test sequences.
Overdriving digital drivers without strict pulse limits risks permanent device destruction.
Consider a modified bus structure where an 8-bit non-inverting driver feeds an unprobed intermediate bus through trace jumpers. To verify logic continuity without direct bed-of-nails contact on jumper nets, the vector generator overdrives the input enable line while applying forced high and low states to upstream bus drivers. The backdrive thermal limit calculation evaluates total energy dissipation using the integrated current integral:
E = integral from 0 to t_pulse of (V_cc – V_sat) I_backdrive dt
Assuming a supply voltage of 3.3 volts, a saturation voltage drop of 0.4 volts, an average backdrive current of 220 milliamperes, and a synthesized pulse width of 1.5 milliseconds, the total energy deposited into the output driver junction during a single vector pulse calculates as follows:
E = (3.3 V – 0.4 V) 0.220 A 0.0015 s = 0.000957 Joules = 0.957 millijoules
If vector synthesis requires 16 consecutive patterns to test all bus permutations without cooling pauses, cumulative thermal energy reaches 15.3 millijoules. The resulting junction temperature rise exceeds 45 degrees Celsius above ambient, pushing the silicon past safe operating thresholds. The vector synthesis tool must insert 10-millisecond delay vectors between excitation pulses ~ extending execution time, but protecting silicon integrity.
Cluster test vectors replace direct contact excitation when physical access drops below single-probe node coverage.
Algorithmic Pattern Generation for Partial Access Nets
When physical probes contact only a fraction of net nodes, automatic pattern synthesis tools compute state transitions from upstream logic propagation. Partial-access synthesis uses Boolean satisfiability algorithms to construct input stimulus sequences that expose internal net faults at downstream scannable registers or accessible probe points.
Automatic test pattern generation (ATPG) software models modified logic paths as binary decision diagrams. The vector generator propagates logic low and high states from available boundary-scan pins or remaining probe contact pads, checking whether a short circuit to an adjacent net creates an observable fault.
Synthesis engines encounter specific structural failure modes when processing modified high-density assemblies:
- Unconstrained Bus Contention ~ Synthesized vectors drive opposing logic levels onto shared parallel nets, damaging driver output stages.
- BSDL Register Mismatch ~ Device firmware re-flashes alter boundary cell length without updating boundary scan definition files.
- Backdrive Timeout Violations ~ Extended excitation sequences test unprobed logic clusters without thermal pauses.
- False Positive Opens ~ Layout trace impedance shifts attenuate high-speed vector edge transitions below sensing thresholds.
- Diagnostic Ambiguity Expansion ~ Lost physical probe points prevent isolating short circuits to individual component pins.
Dynamic software algorithms can partially compensate for missing test pads, but loss of physical access inevitably degrades diagnostic resolution.


Yield
Defect rates on modified high-density assemblies correlate directly with structural test coverage during production ICT. Modifications like manual trace cuts, bodge wires, and fine-pitch BGA rework introduce mechanical failures including solder bridges, insufficient reflow, damaged traces, and lifted pads. Vector synthesis restores fault isolation on boards where physical probe density drops below standard manufacturing limits.
Fault Dictionary Synthesis and Diagnostic Depth
Automated diagnostic engines rely on pre-computed binary matrices that map specific node logic responses to individual circuit failures. When assembly modifications change net topology, the baseline fault dictionary becomes obsolete. Vector re-synthesis updates the dictionary by simulating single-stuck-at faults, solder bridge combinations, and open circuits across all modified nets.
Diagnostic depth measures a system’s ability to isolate a failure to a specific component, pin, or net segment. While direct physical probing achieves single-pin resolution, relying on partial node access or cluster boundary scan reduces diagnostic depth from a single pin to a cluster of components. Vector optimization algorithms attempt to shrink these diagnostic groups by generating finer pattern sequences.
Without physical access, structural test coverage drops significantly across modified nets.
| Modification Type | Physical Access Reduction | Solder Short Sensitivity | Trace Open Sensitivity | Diagnostic Isolation Depth |
|---|---|---|---|---|
| Trace Cut and Jumper Bodge Wire | 10% to 20% Net Loss | 94.2% Coverage | 88.0% Coverage | Net Pair or Jumper Segment |
| Fine-Pitch BGA Respin (0.4mm to 0.35mm) | 30% to 50% Net Loss | 81.5% Coverage | 72.4% Coverage | Component Package Boundary |
| Micro-Via Layer Stack Addition | 15% to 25% Net Loss | 89.0% Coverage | 85.1% Coverage | Sub-Surface Net Node |
| Chiplet / SiP Integration ECO | 60% to 85% Net Loss | 62.3% Coverage | 54.0% Coverage | Multi-Chip Functional Block |
Stale BSDL models cause most test vector synthesis failures during assembly modifications.

Pseudo-Functional Testing for Blind Node Isolation
Unprobed circuit nodes behind physical cuts or jumpers require dynamic stimulation to verify signal integrity. Pseudo-functional vector synthesis generates clocking cycles and register shifts to verify sub-circuit operation without converting the ICT system into a full functional tester.
Adding pseudo-functional routines to structural ICT programs fills coverage gaps created by missing probe access. The synthesis engine applies resets, loads configuration registers over available serial or parallel buses, and checks that outputs transition within expected voltage and timing windows. This hybrid approach preserves defect detection while keeping vector development costs manageable.
Verifying test vector program integrity after assembly modifications requires a methodical quality decision checklist:
- Netlist Hash Matching ~ Confirms post-modification CAD extraction hashes match the netlist imported into the synthesis software suite.
- BSDL Syntax Compliance ~ Verifies all scannable silicon BSDL files pass IEEE 1149.1 syntax checks after device package revisions.
- Backdrive Thermal Bounds ~ Ensures no synthesized vector holds a forced overdrive state longer than 2.0 milliseconds continuously.
- Coverage Threshold Audit ~ Validates structural fault coverage across modified nets stays above contractual minimums.
- Golden Board Execution ~ Confirms generated test vectors pass 50 consecutive execution loops on a verified physical assembly without false failures.
When a modified circuit net loses direct physical probing access, combining boundary scan cluster testing with functional boundary stimulation ensures test program stability.
Lien
Commercial scope boundaries in high-density modifications often obscure who is responsible when structural test coverage drops between design houses and contract manufacturers. When an ECO alters board access, disputes arise over who pays for vector re-synthesis, fixture plate rework, and flying probe adjustments. A solid turnkey transfer contract defines explicit structural test deliverables to prevent delays during factory retooling.

Contractual Deliverables in Vector Re-Synthesis Scope
Engineering change statements of work define file formats, structural coverage thresholds, and fixture rework obligations. When submitting an assembly modification package to a turnkey manufacturing partner, the documentation scope extends beyond revised Gerber and fab files to include revised netlist extractions, updated BSDL models for new IC variants, ATPG source vector files, and revised fault coverage reports.
Vector re-synthesis demands specialized test engineering time. Turnkey contracts set specific acceptance criteria for modified test programs, such as a maximum false-failure rate (typically under 0.1%) and a minimum structural fault coverage floor (typically 85% for partial-access designs). If physical access limits from buyer layout changes push coverage below that floor, the engineering change order allocates additional hours for flying probe augmentation or custom cluster test development.
Unplanned fixture modifications quickly drive up tooling costs.

Fixturing Engineering Hours and Amortization Mechanics
Modifying physical bed-of-nails plates requires mechanical drilling, wire repositioning, and probe receptacle insertion. These fixture modifications run between $1,500 and $6,000 per revision, depending on how many test pins move and the target pin pitch. Reprogramming flying probe software requires less hardware rework, but demands engineering hours to re-synthesize vectors and optimize probe trajectories.
| Engineering Work Element | Turnkey Scope Hours | Semi-Custom Scope Hours | Typical Cost Range (USD) | Primary Deliverable |
|---|---|---|---|---|
| CAD Netlist Delta Extraction & Reconciliation | 4 to 8 Hours | 2 to 4 Hours | $600 to $1,200 | Reconciled Netlist Database |
| BSDL File Parsing & IEEE Syntax Validation | 3 to 6 Hours | 1 to 3 Hours | $450 to $900 | Validated BSDL File Set |
| Vector Re-Synthesis & ATPG Generation | 12 to 24 Hours | 6 to 12 Hours | $1,800 to $3,600 | ATPG Vector Executable File |
| Backdrive Thermal Simulation & Safety Audit | 6 to 12 Hours | 2 to 6 Hours | $900 to $1,800 | Thermal Analysis & Vector Delay Log |
| Fixture Plate Mechanical Rework & Re-Wire | 16 to 32 Hours | 8 to 16 Hours | $2,400 to $4,800 | Physical Test Fixture Hardware |
| Golden Board Proofing & Coverage Reporting | 8 to 16 Hours | 4 to 8 Hours | $1,200 to $2,400 | Signed Coverage Audit Dossier |
Engineering teams that formalize vector re-synthesis deliverables alongside layout modifications establish clear financial accountability and preserve manufacturing quality across assembly revisions.