Free Space Quasi Optical Transmission Loss Calibration for Radome Materials
Calibrate free-space quasi-optical benches with time-gated TRL standards to prevent radome transmission loss from breaching radar EIRP regulatory limits.

Focus
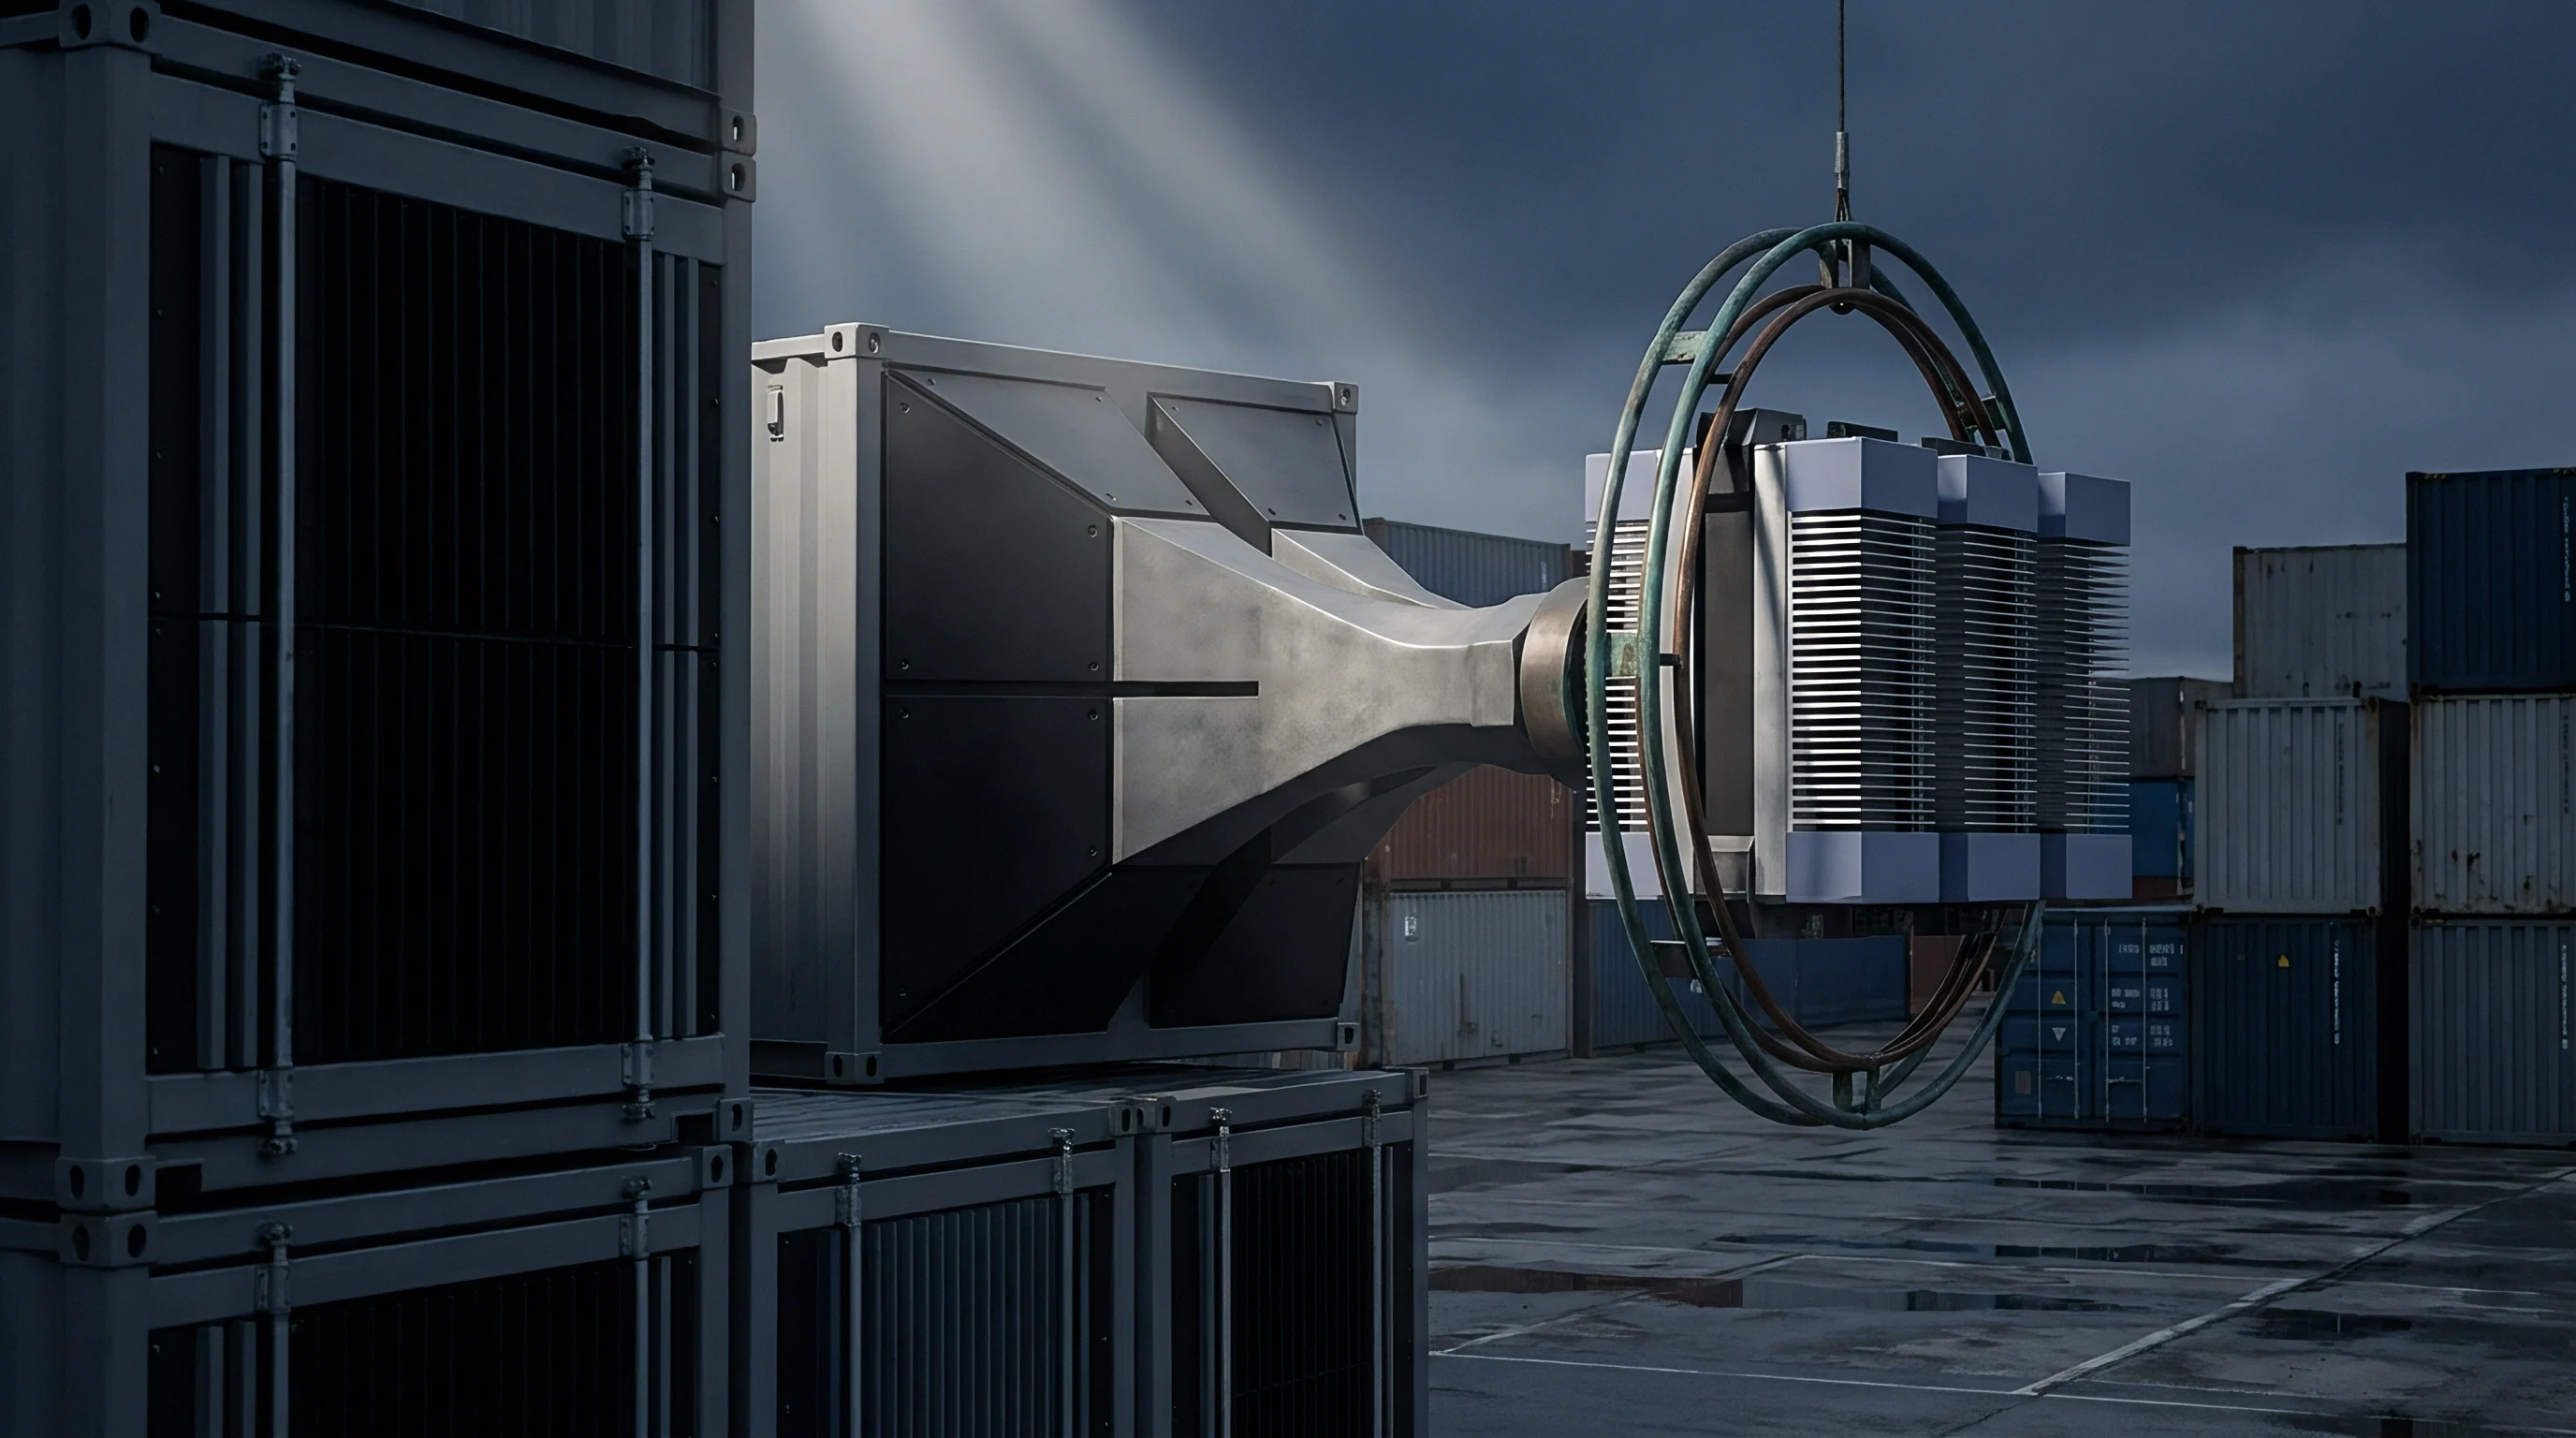
Millimeter-wave radar enclosures introduce transmission loss, reflection ripples, and wavefront distortion that directly alter equivalent isotropically radiated power and beam pointing accuracy. Planar radome coupon testing relies on quasi-optical benches to measure the complex scattering parameters of low-loss dielectric slabs without the boundary condition errors typical of metallic waveguides or coaxial fixtures. A pair of corrugated conical horn antennas coupled with precision bi-convex or plano-convex PTFE or high-density polyethylene lenses creates a Gaussian beam waist at an intermediate sample plane.
Placing the flat radome material sample at this beam waist positions the material in a planar wavefront environment that mimics far-field propagation across automotive radar frequencies from 76 GHz to 81 GHz as well as 60 GHz WiGig bands.
Rayleigh distance governs the longitudinal clearance between each dielectric lens and the sample plane. Aligning the focal points requires millimeter accuracy along the optical axis to prevent wavefront curvature from skewing insertion loss calculations. A sample diameter of at least three to four times the beam waist radius prevents beam spillover around the coupon edges, which otherwise generates edge diffraction spikes that distort transmission measurements.
Clamping fixtures must hold the sample strictly perpendicular to the incident propagation axis for normal incidence evaluations, or rotate along a precision goniometer track for transverse electric and transverse magnetic polarization sweeps across oblique angles.
Coupled dielectric lenses collimate divergent horn emissions into paraxial Gaussian beams that illuminate planar test specimens without metallic wall contact.
Precise mechanical fixturing fixes the repeatability of free-space transmission coefficient extraction:
- Corrugated horn feeds suppress higher-order waveguide modes to maintain circular beam symmetry across the entire waveguide frequency band.
- Collimating dielectric lenses convert spherical phase fronts into flat phase surfaces across the intermediate Rayleigh region.
- Absorbing baffle apertures isolate edge diffraction from corrupting the receiving antenna aperture during high-dynamic-range sweeps.
- Precision linear micrometer rails position the material specimen at the exact beam waist plane to eliminate phase curvature offsets.
- Goniometric sample holders establish precise angular indexing during oblique transverse electric and transverse magnetic insertion loss sweeps.
Vector network analyzer drift ruins sub-terahertz insertion loss measurements when ambient temperatures fluctuate during long test sequences. High-frequency coaxial cables running from the frequency extension modules to the horns undergo phase shifts when physically displaced. Rigid bench configurations anchor the extension heads directly to an optical breadboard, keeping the transmission path fixed.
Calibration planes establish the reference phase and amplitude baseline before introducing the sample into the path. Under supply contract stipulations matching automotive radar quality standards, suppliers must deliver raw S-parameter transmission traces with documented ambient bench temperature logs within two degrees Celsius to validate baseline drift stability.

Extraction
Vector error correction in free space requires establishing reference planes without the physical mechanical standards used in coaxial lines. Thru-Reflect-Line procedures eliminate systematic errors caused by horn reflections, lens absorption, and internal bench multipath. The calibration begins with an unimpeded transmission path serving as the thru standard.
A metal plate with an optical mirror finish acts as the high-reflection standard, reflecting incident energy back toward the transmitting horn. Moving the receiving stage or the reference mirror by a quarter wavelength establishes the line standard, providing phase diversity across the operational band.
Free space calibration executes across a sequence of discrete physical steps:
- Align the transmit and receive horn-lens assemblies along the optical rail until transmission magnitude peaks and reflection phase exhibits planar symmetry.
- Acquire the through calibration baseline across the full sweep band with an empty sample holder to establish the unattenuated reference level.
- Mount an aluminum plate of known surface roughness at the sample reference plane to capture the unity-reflection vector.
- Offset the receiving stage along the optical axis by an odd quarter-wavelength increment to supply the line reference condition.
- Compute the twelve-term systematic error model within the vector network analyzer firmware to correct raw scattering parameter acquisition.
Multipath interference within the bench optics creates residual ripple in the calibrated transmission coefficient. Internal reflections bounce between the horns, the lens surfaces, and the front and back interfaces of the sample. Time-domain gating isolates the direct transmission path by applying an inverse Fourier transform to the frequency-domain data, windowing out delayed multipath spikes, and transforming the direct path back to the frequency domain.
A twenty-picosecond gate span cleanly strips secondary lens reflections while preserving the fundamental dielectric material response across 77 GHz.
Excessive time-domain gate suppression truncates genuine internal multiple reflections inside thick radome panels, falsifying the extracted loss tangent. Fabry-Pérot resonance within low-loss plastics creates physical transmission peaks and nulls based on sample thickness and real permittivity. If gating suppresses these genuine internal reflections, the mathematical extraction algorithm overestimates dielectric attenuation.
The test engineer balances the filter gate width against the electrical thickness of the specimen. Real permittivity and dielectric loss tangent derive from inversion algorithms matching the complex transmission coefficient to planar Fresnel boundary equations.
The mathematical extraction resolves material parameters from measured transmission data across candidate radome polymers:
| Material Designation | Real Permittivity | Loss Tangent | One-Way Insertion Loss at 1.5 mm Thickness | Thermal Expansion Coefficient |
|---|---|---|---|---|
| Polytetrafluoroethylene | 2.04 | 0.0004 | 0.12 dB | 135 ppm/K |
| Cross-Linked Polystyrene | 2.53 | 0.0007 | 0.24 dB | 65 ppm/K |
| Polycarbonate | 2.78 | 0.0090 | 1.45 dB | 70 ppm/K |
| Polyetherimide | 3.15 | 0.0060 | 1.28 dB | 55 ppm/K |
| Acrylonitrile Butadiene Styrene | 2.65 | 0.0085 | 1.36 dB | 85 ppm/K |
| Fused Silica | 3.82 | 0.0001 | 0.18 dB | 0.5 ppm/K |
Phase retrieval accuracy dictates real permittivity precision. A quarter-wave displacement error during the calibration line standard translates directly into an artificial phase slope across the sweep. Surface roughness on the radome coupon also introduces diffuse scatter that manifests as non-recoverable transmission attenuation.
Material coupons must be prepared with surface planar parallel tolerance exceeding five micrometers. Mechanical thickness variation across the illuminated spot directly distorts phase calculation.
Stable benches reveal true material loss when optical components remain completely stationary throughout the entire measurement cycle.
Boresight
Antenna pattern integration transforms raw radome coupon transmission loss into vehicle-level performance margins. When radar sensors sit behind painted front bumpers or decorative brand emblems, the radome functions as the exterior electromagnetic window. Insertion loss reduces the radar maximum detection range according to radar range equation quartics, where a 1 dB one-way insertion loss strips more than 10 percent of radar operational range.
Inhomogeneous material density, molded knit lines, and variable wall thickness bend the advancing phase front, deflecting the antenna beam off its physical boresight axis.
ETSI EN 301 091 defines radiated spectral limits, spurious emission masks, and transmitter equivalent isotropically radiated power ceilings for 76 GHz to 81 GHz radar equipment in the European Union. In the United States, FCC Part 95M sets strict radiated power boundaries and occupied bandwidth limits. When an automotive supplier alters the radome material blend or adds metallic flake paint layers, the altered transmission loss degrades the certified radiated power profile.
A drop in radiated field strength below type-approval thresholds demands permissive change filings or complete sensor re-certification.

Are Symmetrical Sandwich Geometries Immune to Wavefront Distortion?
Balanced multilayer radomes cancel internal reflections across specific incident angular spreads. A classic solid half-wavelength radome wall provides zero reflection at a single design frequency and incidence angle, yet exhibits sharp transmission drops across wider manufacturing tolerances or temperature extremes. Sandwich structures incorporate low-density foam or honeycomb cores bounded by thin, dense thermoplastic skins to minimize weight while holding structural rigidity.
| Wall Architecture | Typical Thickness | Transmission Efficiency | Boresight Error Shift | Compliance Risk Under ETSI EN 301 091 |
|---|---|---|---|---|
| Monolithic Half-Wave Slab | 1.18 mm | 96.5% | 0.08 deg | Low risk when molding tolerances hold within 20 micrometers |
| Thin-Wall Monolithic | 0.30 mm | 98.2% | 0.03 deg | Structural failure under stone impact forces material thickening |
| A-Sandwich Core and Skins | 3.45 mm | 92.0% | 0.25 deg | Core density variation induces side lobe mask violations |
| C-Sandwich Multilayer | 5.80 mm | 89.5% | 0.42 deg | Phase front curvature exceeds automotive tracking limits |
Multilayer structures introduce complex internal interfaces where adhesive layers degrade overall insertion efficiency. Core density variations across large automotive bumper fascia cause local phase shifts that distort the radar antenna side lobes. Elevated side lobes breach regulatory spectral emission masks, scattering spurious energy into adjacent automotive azimuth sectors.
A compliance failure in side lobe suppression halts vehicle end-of-line certification.
Will Temperature Shifts Invalidate Factory Permittivity Grants?
Thermal excursions alter thermoplastic dielectric constants by expanding molecular lattices and shifting dipole relaxation frequencies. Automotive radomes must endure ambient conditions from minus forty degrees Celsius to plus eighty-five degrees Celsius. As the radome warms under direct sunlight or engine compartment soak, the real permittivity of typical polycarbonate blends drops, shifting the tuned half-wave resonance away from 77 GHz.
The resulting phase lag steers the radar boresight by tenths of a degree, creating phantom obstacle bearings within autonomous emergency braking algorithms.
Annex B of ETSI EN 301 091 mandates radiated power measurement across operational temperature boundaries where thermal detuning directly reduces transmitter field strength.
Paint systems layered onto radomes compound dielectric attenuation. Automotive exterior finishes apply conductive metal-oxide particles to achieve metallic visual effects. These metallic coats create conductive dissipation surfaces that convert millimeter-wave radiation into heat.
Primer, base coat, and clear coat layers must undergo individual quasi-optical transmission calibration to establish their compound complex permittivity. Uncontrolled paint application transforms an approved sensor housing into a non-compliant attenuator that invalidates initial grant approvals.
Uncalibrated radome absorption lowers sensor antenna gain, cuts receiver sensitivity, and forces costly complete system re-testing when field vehicles fail baseline road qualification checks.

Yield
Production economies depend on tight molding parameters to preserve millimeter-wave transparency across thousands of parts per week. An injection-molded radome changes electrical thickness as tooling cavities wear or injection pressures drift. Variations in injection barrel melt temperature cause localized polymer orientation, leading to dielectric anisotropy.
Sourcing teams cannot assume that raw resin specification sheets accurately reflect millimeter-wave properties, because material suppliers frequently report permittivity measured at 1 MHz or 1 GHz using low-frequency capacitance fixtures.
Establishing incoming inspection protocols on factory shipments demands coupon-level sample testing before parts move to paint lines. A designated five-point sample sweep across each production lot identifies resin density shifts before expensive molding operations begin. If incoming resin displays a loss tangent increase of 0.002 above baseline, total system insertion loss climbs by nearly half a decibel.
That change consumes the entire link budget margin budgeted for bumper curvature and road mud accumulation.
Tooling wear shifts physical radome wall thickness across production runs faster than resin chemistry variations alter baseline permittivity.
Procurement teams protect project schedules by locking transmission loss acceptance criteria into initial tooling purchase agreements. Contract language dictates that production tooling sign-off requires quasi-optical validation across five tooling sample shots per cavity. Sourcing specifications establish maximum acceptable insertion loss limits of 0.8 dB across 76 GHz to 81 GHz at normal incidence.
Failure to enforce high-frequency dielectric criteria during tool qualification transfers the cost of re-tooling to the automotive Tier 1 integrator after mass production starts.
Laboratory testing schedules introduce lead-time bottlenecks during product launch windows. Accredited millimeter-wave chambers and quasi-optical test benches require advance booking of four to six weeks. Test houses bill approximately three thousand dollars per shift for calibrated quasi-optical material characterization.
When a coupon fails insertion loss limits, re-formulating the polymer blend or cutting down tool steel adds eight to twelve weeks to the launch calendar. Cross-border component imports without documented radome transmission loss certificates risk retention at customs checkpoints when target markets demand verified conformity dossiers.
How far can high-volume resin compounding tolerate recycled regrind additions before local phase jitter triggers an unrecoverable breach of regulatory transmitter masks?